Choosing the right Shot Blasting Steel Wire is not a simple matter of selecting the hardest or cheapest option. The correct wire must match the machine, workpiece, surface condition, and required finish. A wire that performs well on cast iron may damage aluminum parts. The wrong diameter can also create unstable flow, uneven cleaning, or excessive dust.
Dr. David Kirk, a recognized specialist in shot peening, explains, “Shot peening is a cold working process in which the surface is bombarded with small spherical media.” This principle highlights an important point: media shape, size, and consistency directly influence surface results. For blasting applications, buyers should examine carbon content, tensile strength, hardness, straightness, cutting quality, and resistance to breakage. Wire cut into uniform lengths usually provides more predictable coverage than irregular fragments.
Real-world selection requires more than a product data sheet. Ask for test certificates, production details, and evidence from similar applications. Check whether the wire creates acceptable anchor profiles without removing too much base material. Observe the spent media after a trial. Excessive fines may indicate premature wear or poor quality. Still, no selection guide can replace a controlled test on the actual machine. This is where many recommendations become too confident.
Start with a small batch. Measure cleaning efficiency, surface roughness, consumption, and equipment wear. Then compare the total operating cost, not only the purchase price. The “best” Shot Blasting Steel Wire is not always the hardest. It is the one that delivers stable results, protects the workpiece, and remains economical under real production conditions. Mistakes happen. Careful testing makes them less expensive.
Identify the Surface Preparation Requirements
How to Choose the Right Shot Blasting Steel Wire?
Identify the Surface Preparation Requirements
Start with the coating specification, not the abrasive catalogue. Define the required cleanliness grade, surface profile, substrate condition, and final coating thickness. ISO 8501-1 grades such as Sa 2½ require near-white metal cleaning, but visual cleanliness alone is insufficient. Chloride, oil, and dust can remain inside surface valleys.
Match the steel wire abrasive to the required profile. Larger, harder wire creates a more aggressive impact and deeper texture. Smaller wire produces a finer profile and may reduce excessive metal removal. Cut wire begins with sharper edges, while conditioned wire gradually becomes more rounded. This difference affects cleaning speed, profile uniformity, and abrasive consumption. A 50–75 micrometre profile may suit many protective coating systems, but the project specification must control the final decision.
The NACE IMPACT study estimated that corrosion costs the global economy about 2.5 trillion US dollars annually. That figure shows why surface preparation deserves engineering attention, not guesswork. Field inspectors should verify the profile with a replica tape or suitable gauge, then measure soluble salts and dust before coating. A bright surface can still fail.
One practical warning: harder is not always better. Excessive impact can deform thin steel, embed debris, or create a profile that the coating cannot cover. I would review the first blasted test panel before approving full production. Sometimes the initial abrasive choice looks efficient, but the rework tells a different story.
Compare Steel Wire Types and Material Properties
How to Choose the Right Shot Blasting Steel Wire?
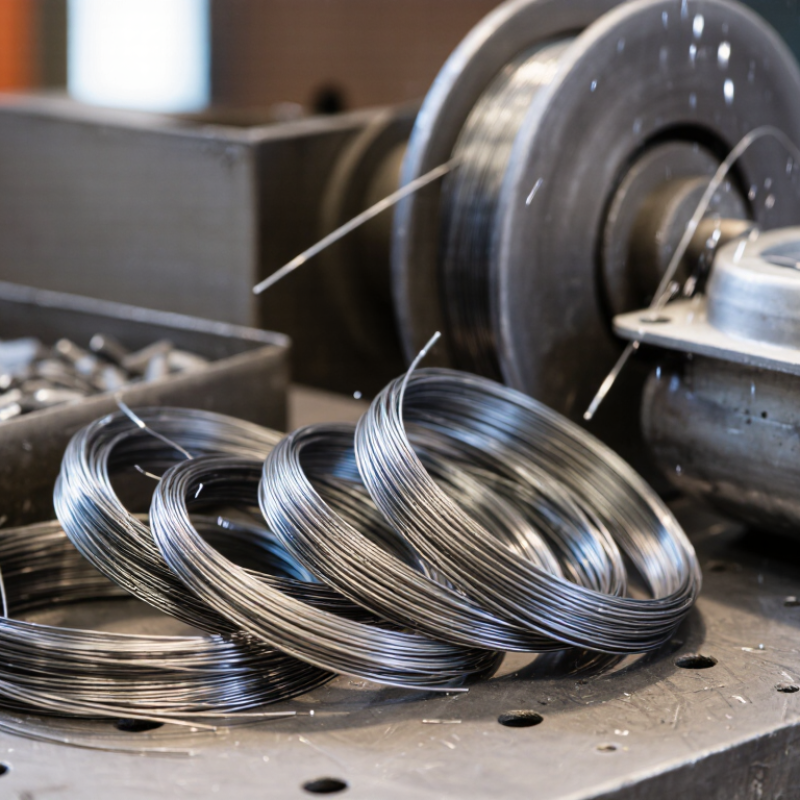
The right wire depends on the surface, machine, and cleaning target. Steel wire types behave differently under repeated impact. High-carbon steel wire offers strong hardness and wear resistance. It suits heavy scale removal from castings and structural parts. However, excessive hardness can increase surface stress and premature wire breakage.
Low-carbon steel wire is softer and more forgiving. It may work better for light cleaning or delicate components. Its service life can be shorter, especially against thick rust. Stainless steel wire resists corrosion and avoids iron contamination on stainless or nonferrous surfaces. It usually costs more, so its material benefit should justify the expense. Wire diameter also matters. Thin wire reaches small recesses, while thicker wire delivers stronger impact. Check hardness, tensile strength, ductility, and fatigue resistance together. One value cannot predict actual performance.
Tips: Start with a small production trial. Record cleaning time, surface profile, dust level, and wire consumption. Inspect the workpiece under proper lighting. A shiny surface is not always a correctly prepared surface. Adjust wheel speed and feed rate carefully. Operators often blame the wire when settings cause the real problem. I have found that practical testing beats a purely theoretical selection. Still, trial results can vary with moisture, part geometry, and machine condition. Keep those variables in your notes.
How to Choose the Right Shot Blasting Steel Wire?
Comparison of representative mechanical properties for commonly used steel wire types in shot blasting applications.
High-carbon steel wire generally provides the highest hardness and tensile strength, making it suitable for demanding cleaning and descaling work. Low-carbon steel wire is more ductile and is often selected when lower impact intensity is preferred. Stainless steel wire offers corrosion resistance and moderate mechanical strength for applications where surface contamination must be minimized. Values shown are representative mid-range figures; actual properties vary with alloy grade, wire diameter, heat treatment, and manufacturing condition.
Select the Correct Wire Diameter and Cut Length
Choosing shot blasting steel wire starts with two practical dimensions: wire diameter and cut length. Diameter controls impact energy, coverage, and surface pressure. Thicker wire hits harder and lasts longer, but it may mark thin castings. Fine wire reaches narrow corners and creates a smoother profile. It also wears faster. In a workshop, I compare the target material, part thickness, and required surface finish before selecting a size. Guessing from visual appearance alone is unreliable.
Cut length changes how the media moves through the blast stream. Short-cut wire spreads quickly and can clean irregular surfaces with fewer deep impacts. Longer cuts deliver stronger, more directional contact, especially on heavy steel components. A useful starting point is a near-equal cut length and diameter, but this is not a fixed rule. Machine wheel speed, air pressure, loading rate, and part geometry can shift the result. Measure the wire with calipers, then inspect the surface under bright light. Look for missed scale, rounded edges, or unwanted dents.
Record the setting that produced the best balance. Keep the batch consistent. Mixing noticeably different diameters can make cleaning uneven and complicate wear tracking. One honest limitation remains: the first selection may be wrong. Trial runs on sample pieces are safer than changing a full production load. Check dust, broken wire, and surface roughness after each test. Small adjustments often outperform a dramatic change.
Match Wire Specifications to Blasting Equipment
Choosing shot blasting steel wire starts with the machine, not the surface. Wheel blasting needs consistent diameter, hardness, and flow. Air blasting demands closer control because nozzle pressure changes impact energy. ISO 11124-3:2018 classifies cast-steel abrasives by chemical and mechanical requirements, giving buyers a reliable specification baseline. For cut wire, match the wire diameter to the equipment’s abrasive valve and nozzle. Oversized particles may bridge the feed system. Fine particles can disappear quickly through the separator.
Measure the working conditions. Many air-blast systems operate around 0.6–0.8 MPa at the nozzle, but actual pressure depends on hose length and nozzle wear. The U.S. Department of Energy’s 2022 Manufacturing Energy and Carbon Footprints report notes that compressed air can represent roughly 10–30% of industrial electricity use. That figure makes abrasive flow and pressure worth checking, not guessing. Lower density wire may reduce impact, even when the pressure gauge looks correct.
In practical trials, I compare surface profile, media breakdown, and dust after one production shift. A wire diameter of 0.6 mm may suit light cleaning, while 1.0 mm or larger can support heavier scale removal. These are starting points, not universal rules. The first setting is rarely right. I also inspect the separator screen weekly, because worn wire changes the mix faster than expected. A little humility helps. Overly hard wire may clean quickly, yet it can increase equipment wear and leave an uneven profile.
Test Blasting Performance and Adjust Operating Parameters
How to Choose the Right Shot Blasting Steel Wire?
Test blasting performance before changing the steel wire grade.
Record surface profile, cleaning time, abrasive consumption, and dust levels. A practical trial should use identical parts, nozzle distance, and exposure time. ISO 11125-4 requires metallic abrasives to meet defined particle-size distributions, so sieve results matter more than nominal wire diameter. A 0.8 mm wire may clean faster, but it can produce a rougher profile and higher impact energy. Measure the profile with a replica tape or digital gauge. The target must match the coating specification, not personal preference.
Adjust operating parameters in small steps.
Keep wheel speed, feed rate, and blast angle stable during comparison. The U.S. EPA AP-42 emission-factor report identifies abrasive blasting as a particulate-emission source, making dust collection performance an important operating check. Track filter pressure and visible dust, not only production speed. Many facilities start near 70–80 m/s wheel speed, then adjust after inspecting edges and recessed areas. Lower speed can reduce wire breakage. Higher speed may shorten cleaning time, but excessive energy wastes media and damages thin sections. ASTM G65 wear-testing principles can help compare durability, although shop conditions rarely match laboratory results. That limitation deserves attention. A short trial can mislead when broken wire, humidity, or poor separation changes the result.
FAQS
Define cleanliness, surface profile, substrate condition, and coating thickness. A bright surface is not enough. Check salts, oil, and dust inside surface valleys.
Larger, harder wire creates stronger impacts and deeper profiles. Smaller wire creates finer textures and removes less metal. The wrong size can cause dents.
A 50–75 micrometre profile suits many protective coating systems. The project specification must control the final target. Do not rely on appearance alone.
Diameter controls impact energy, coverage, and surface pressure. Cut length changes media movement and contact direction. Near-equal length and diameter can be a starting point.
Usually not. Thick wire may mark thin castings or deform light sheet. Fine wire reaches corners and creates a smoother profile.
Match wire diameter with the abrasive valve, nozzle, wheel, and separator. Oversized particles may block feeding systems. Fine particles may pass through separators too quickly.
Check nozzle pressure, hose length, nozzle wear, abrasive flow, and loading rate. Many systems operate near 0.6–0.8 MPa. The gauge may not show actual impact energy.
Blast a test panel before full production. Measure the profile with replica tape or a suitable gauge. Inspect dust, broken wire, missed scale, dents, and media breakdown.
No. Harder wire may clean quickly but increase equipment wear. It can also create uneven profiles or embed debris. The first selection may be wrong.
Conclusion
Choosing the right Shot Blasting Steel Wire begins with clearly defining the surface preparation requirements, including the material, coating or contamination to be removed, desired surface profile, and acceptable finish. Different steel wire types offer varying levels of hardness, toughness, durability, and resistance to fatigue, so the selected material should balance cleaning efficiency with service life. Wire diameter and cut length also influence impact strength, coverage, and surface texture; finer wire is generally suited to delicate or detailed work, while larger wire can provide more aggressive cleaning.
The wire specifications must be compatible with the blasting equipment, including its wheel or air system, operating capacity, and recovery setup. Before full production, conduct controlled performance tests and adjust factors such as abrasive flow, blasting speed, pressure, exposure time, and workpiece distance. Monitoring surface quality, wear, dust, and equipment performance helps confirm the best combination and maintain consistent results.
 Hanshen